
 ISO 9001:2015 & QCI Approved
STP and ETP Plant Manufacturer in Silchar
Trity Environ Solutions is a leading STP and ETP plant manufacturer in Silchar, engineering turnkey wastewater treatment systems for Meherpur, Ramnagar industrial corridor, and tea processing units. We build heavy-duty effluent treatment plants and sewage treatment plants engineered for strict PCBA compliance across the Barak River basin, backed by pan India installation support.
PCBA / CPCB Norm Compliant
Heavy Fabrication
Engineering Environmental Compliance and Water Recovery in Silchar's Industrial Corridor
Silchar holds a pivotal position in Assam's economy, supporting extensive manufacturing across Meherpur Industrial Estate, Panchgram paper zone, and Ramnagar Industrial corridor. These complexes feature intensive tea processing, paper and pulp manufacturing, agro-commodities, timber processing, and logistics workshops, generating high-volume wastewater streams characterized by organic pulping wastewater, high suspended fibers, tea processing effluent, and municipal commercial sewage.
Discharging untreated or substandard effluent into municipal drains, tidal creeks, or water bodies feeding the Barak River creates severe ecological degradation and attracts immediate enforcement action under PCBA regulations and PCBA and NGT initiatives enforcing strict stoppage of untreated municipal and agro-industrial waste into the Barak River.
Aquifers across Silchar are classified as localized water stress with high mineral content in the Cachar valley. Under strict state environmental policies and Central Ground Water Authority guidelines, industrial enterprises cannot sustain operations on fresh water extraction alone.
Developing a closed-loop wastewater management strategy is vital to safeguard operational continuity. Trity Environ Solutions delivers custom-built effluent treatment plants combining automated chemical coagulation, dissolved air flotation, high-rate lamella settling, and advanced oxidation to eliminate toxic contaminants, lower biological oxygen demand, and reclaim high-grade water for process cooling and boiler feed.
Simultaneously, Silchar's urban expansion across Silchar town, Tarapur, Rangirkhari, Assam University campus, and Silchar Medical College generates heavy daily volumes of domestic blackwater and greywater from hospitals, educational institutions, commercial centers, and residential developments. Untreated sewage disposal violates National Green Tribunal mandates and municipal health norms.
We manufacture modular, odorless, and low-footprint sewage treatment plants based on Moving Bed Biofilm Reactor (MBBR) and Membrane Bioreactor (MBR) technologies. These systems purify raw sewage into clear, hygienic water suitable for toilet flushing, green belt maintenance, and cooling tower makeup, lowering operating costs while ensuring full compliance.
Operating an industrial manufacturing plant in Meherpur Industrial Estate or developing a commercial project in Silchar town? Request a free technical assessment from our environmental engineering team to analyze your raw effluent parameters and design an optimized treatment layout.
WHY THIS SYSTEM?
Key Benefits of STP and ETP Plant Manufacturer in Silchar
Engineered for heavy industrial resilience, groundwater preservation, and reliable PCBA compliance across Silchar.
Custom Chemistry for Silchar's Core Sectors
Engineered specifically to neutralize the complex wastewater generated by tea processing, paper and pulp manufacturing, agro-commodities, timber processing, and logistics workshops across Meherpur Industrial Estate, ensuring complete removal of heavy metals, suspended solids, and toxic chemical residues.
Guaranteed PCBA and CPCB Compliance
Designed to meet or exceed Pollution Control Board of Assam discharge parameters (BOD under 10 mg/L, COD under 50 mg/L, TSS under 10 mg/L), protecting your unit against regulatory notices and closure orders.
High-Recovery Closed-Loop Water Recycling
Integrated ultrafiltration and reverse osmosis stages reclaim 85 to 95 percent of treated wastewater for manufacturing reuse, countering groundwater stress and environmental sensitivity across Silchar.
Compact Footprints for Dense Industrial Plots
Space-efficient modular designs and vertical clarifiers enable factories and commercial buildings in Silchar to install modern wastewater treatment without requiring additional land acquisition.
Dedicated Engineering & AMC Support in Assam
Backed by prompt field service engineers, chemical replenishment, and scheduled preventive maintenance under our comprehensive Annual Maintenance Contracts across Silchar and northeast India.
High-Capacity Effluent Treatment Engineered for Silchar's Core Industries
Industrial wastewater from tea processing, paper and pulp manufacturing, agro-commodities, timber processing, and logistics workshops in Meherpur Industrial Estate, Panchgram paper zone, and Ramnagar Industrial corridor carries severe chemical complexity that standard biological plants cannot break down. Effluent streams contain organic pulping wastewater, high suspended fibers, tea processing effluent, and municipal commercial sewage, which rapidly foul biological media and cause severe equipment wear if not properly pre-treated. Overcoming these challenges requires multi-stage physico-chemical and mechanical treatment.
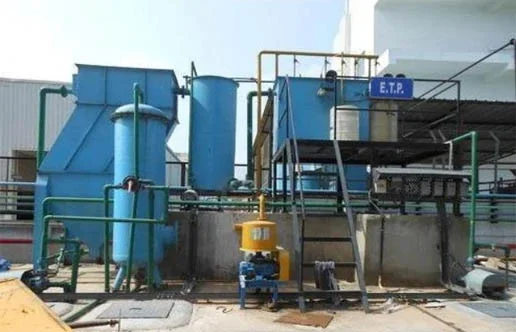
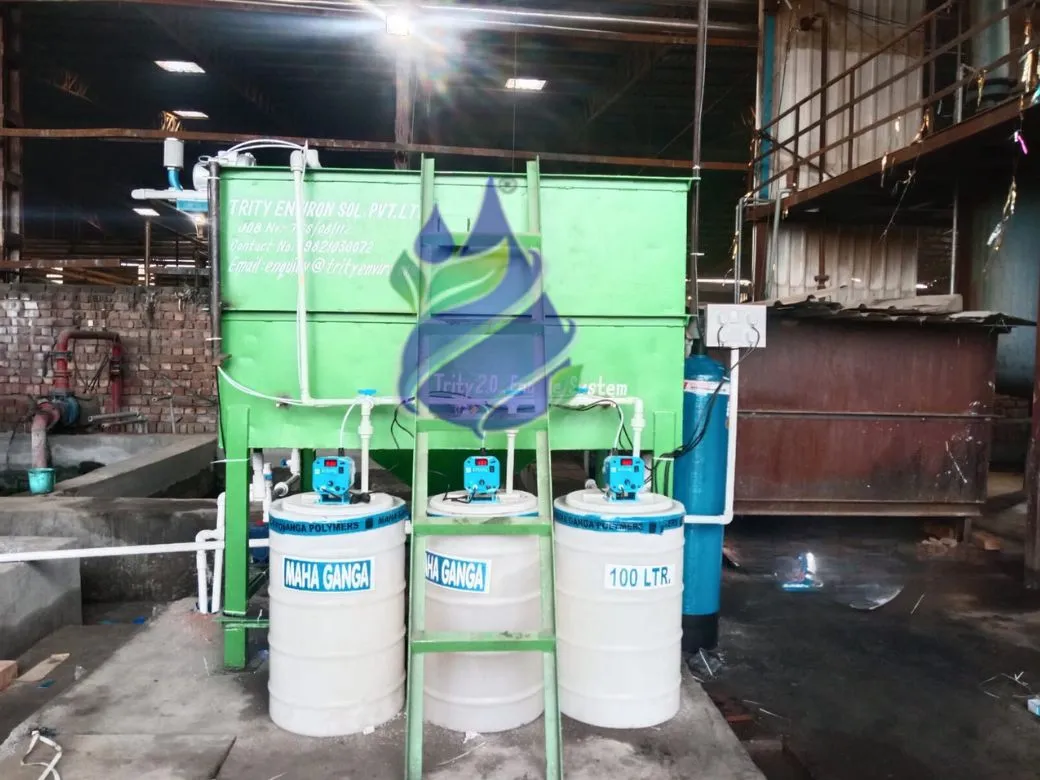
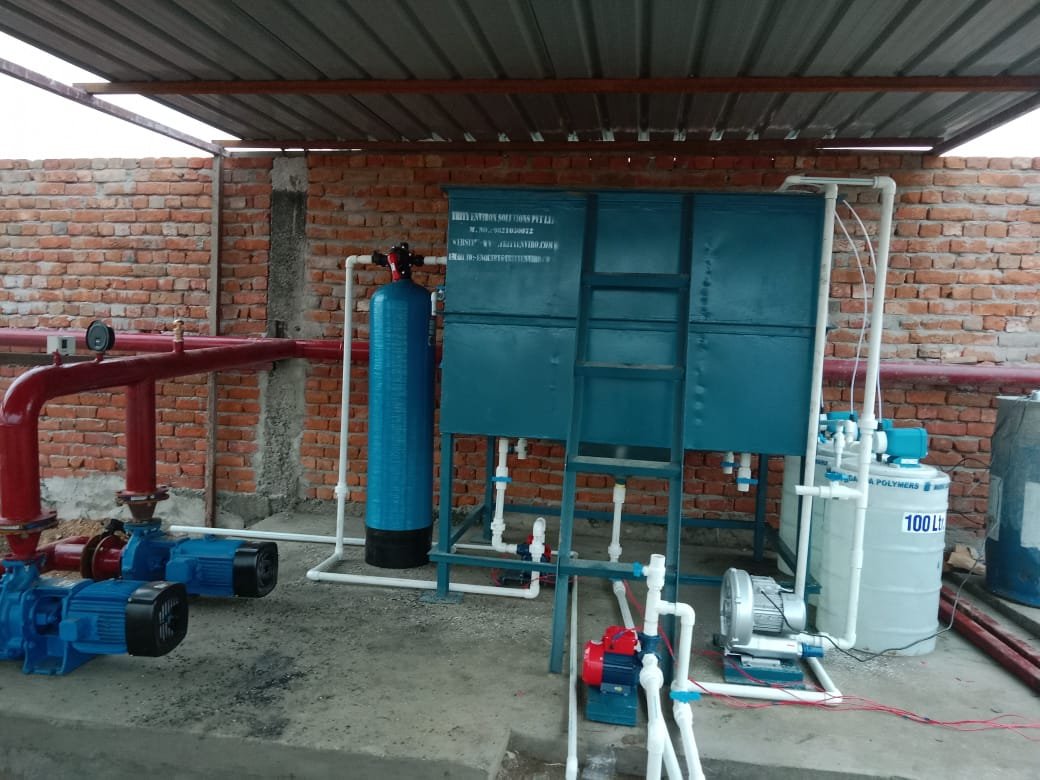
Trity Environ Solutions manufactures primary treatment systems featuring automated bar screens, grit removal, and mechanical oil skimmers to capture free and emulsified oils. The wastewater flows into flash mixing and flocculation chambers where automated dosing pumps introduce coagulants, polyelectrolytes, and pH-correcting reagents. Our lamella clarifiers and vertical tube settlers ensure rapid solids separation within a compact structural footprint.
Settled sludge is processed through recessed plate membrane filter presses, creating dry cake for authorized hazardous waste management. For facilities handling refractory COD, toxic solvents, or heavy metals, we integrate chemical oxidation, Fenton reactors, and activated carbon polishing columns to ensure full discharge compliance.
Decentralized Commercial Sewage Treatment for Silchar's Urban Infrastructure
Rapid urban growth across Silchar town, Tarapur, Rangirkhari, Assam University campus, and Silchar Medical College demands dependable, decentralized sewage treatment. Hospitals, hotels, educational campuses, and residential townships face strict regulatory pressure from the PCBA and municipal authorities to ensure zero untreated sewage enters stormwater channels or the Barak River.
Traditional sewage treatment plants suffer from large civil footprints, high power consumption, and persistent odor emissions. Trity Environ Solutions designs prefabricated packaged sewage treatment plants based on Moving Bed Biofilm Reactor (MBBR) and Membrane Bioreactor (MBR) technologies.
In our MBBR plants, virgin polypropylene media remain in suspension via fine bubble diffusers, creating resilient biomass capable of handling sharp load fluctuations.
For facilities requiring the highest effluent clarity and minimal footprint, our MBR plants combine biological digestion with submerged 0.04-micron membrane filtration. The permeate is crystal clear, odorless, and pathogen-free, immediately reusable in central HVAC cooling towers, toilet flushing, and greenbelt irrigation. Every plant is supported by an Annual Maintenance Contract. Consult our engineering team to evaluate your project needs.
Zero Liquid Discharge (ZLD) to Safeguard the Barak River and Ensure Water Continuity
The Barak River is an essential water source under intensive ecological scrutiny in Assam. Due to extensive industrial discharge, PCBA and NGT initiatives enforcing strict stoppage of untreated municipal and agro-industrial waste into the Barak River. Regulatory agencies are increasingly making Zero Liquid Discharge (ZLD) systems mandatory for water-intensive industries across the region.
Operating a ZLD plant requires thermal and electrical optimization to keep running costs manageable. Trity Environ Solutions engineers energy-efficient closed-loop ZLD systems. Following primary physico-chemical and secondary biological treatment, effluent passes through chemical softening and silica removal before entering multi-stage brackish water reverse osmosis (RO) systems. This membrane phase recovers 85 to 90 percent of clear water for direct return to factory processes.
The concentrated brine stream is processed through high-pressure disc-tube reverse osmosis (DTRO) and thermal Multi-Effect Evaporators (MEE) or Mechanical Vapor Recompression (MVR) systems paired with Agitated Thin Film Dryers (ATFD). Solid salts crystallize into dry cake for safe disposal, leaving zero liquid outflow. This closed loop protects your unit against groundwater extraction limits and ensures uninterrupted manufacturing.
SYSTEM CONFIGURATIONS
Types of STP and ETP Configurations for Silchar
Tailored wastewater treatment technology selected for your effluent chemistry, water reuse needs, and PCBA consent.
Physico-Chemical Industrial ETP for Silchar
Engineered for tea processing, paper and pulp manufacturing, agro-commodities, timber processing, and logistics workshops in Meherpur Industrial Estate. Incorporates mechanical oil skimmers, flash mixing, chemical precipitation, lamella tube settlers, and automated filter presses to remove heavy metals, suspended solids, and chemical residues.
Chemical Oxidation & Heavy Metal Precipitation ETP
Specialized chemical treatment for petrochemical units, chemical plants, and tea factories. Integrates Fenton reaction vessels, pH correction tanks, and chemical precipitation to eliminate refractory COD, toxic solvents, and dissolved metals.
Packaged MBBR & MBR Sewage Treatment Plants (STP)
Engineered for commercial complexes, healthcare facilities, and residential colonies in Silchar town. Delivers compact, odorless biological treatment producing high-purity water safe for toilet flushing and cooling towers.
Zero Liquid Discharge (ZLD) & Membrane Recycling Train
Comprehensive closed-loop water recovery combining dual-media filters, ultrafiltration, high-recovery reverse osmosis, and thermal evaporators (MEE/ATFD). Recovers up to 98 percent of wastewater as pure process water.
Not certain which setup fits your Silchar plant? Schedule a technical consultation with our engineering specialists.
STEP-BY-STEP WORKFLOW
How the STP and ETP Execution Process Works in Silchar
Turnkey engineering from influent lab analysis to fabrication, site erection, and PCBA consent validation in Silchar.
01
On-Site Effluent Characterization & Silchar Regulatory Review
Our environmental specialists visit your plant in Silchar to collect raw wastewater samples, testing parameters including BOD, COD, TSS, TDS, oil content, and heavy metals while reviewing PCBA consent conditions.
02
Custom Process Design and Hydraulic Sizing
We develop detailed P&ID schematics, mass balances, footprint layouts, and electrical automation drawings aligned with your plot constraints and recycling goals.
03
Heavy-Duty Fabrication and In-House Quality Assurance
Pressure vessels, settling tanks, skids, and clarifiers are fabricated using high-grade stainless steel or epoxy/FRP-lined mild steel, followed by rigorous pressure and weld leak testing.
04
Site Installation, Piping Routing & Electrical Automation
Our engineering crew manages site positioning, civil coordination, mechanical pump installations, valve networks, and PLC control panel wiring with minimal interruption to factory operations.
05
Commissioning, PCBA Sampling Verification & AMC Handover
We seed microbial biomass, optimize chemical dosing recipes, conduct performance test runs to verify treated water against PCBA standards, train operating staff, and transition the plant into regular operation under an Annual Maintenance Contract.
COMMON INQUIRIES
Frequently Asked Questions in Silchar
Common questions regarding STP and ETP manufacturing, industrial compliance, water recovery, and PCBA norms in Silchar.
Q1. What are the mandatory PCBA discharge standards for industrial units in Silchar?
The Pollution Control Board of Assam (PCBA) enforces standards aligned with CPCB regulations. For discharge into inland surface waters or drains, treated effluent must generally maintain a pH between 5.5 and 9.0, BOD under 30 mg/L (stricter projects under NGT surveillance require BOD under 10 mg/L), COD under 250 mg/L (or under 50 mg/L for sensitive zones), TSS under 100 mg/L, and Oil & Grease under 10 mg/L. Units located near the Barak River basin are increasingly directed to install Zero Liquid Discharge systems with no liquid bypass.
Q2. Can your ETP systems handle complex chemical effluents generated in Silchar's factories?
Yes. We install specialized multi-stage primary treatment systems comprising automated mechanical oil skimmers, flash mixers, and lamella clarifiers. These units extract floating mineral oils and accelerate the settling of abrasive iron and coal dust before water reaches secondary biological or membrane stages, preventing filter fouling and pump wear.
Q3. How much space is needed for a packaged sewage treatment plant in Silchar?
While older activated sludge systems require over 1,200 square feet for a 100 KLD capacity, our compact Moving Bed Biofilm Reactor (MBBR) systems require only 500 to 700 square feet. For tight commercial premises in Silchar town, our submerged Membrane Bioreactor (MBR) plants occupy under 400 square feet and can be sited in basements or covered parking podiums without odor issues.
Q4. Is treated wastewater from your Silchar plants safe for boiler and cooling tower reuse?
Yes. With our tertiary filtration, ultrafiltration, and reverse osmosis polishing trains, treated wastewater achieves turbidity below 1 NTU, total dissolved solids below 100 ppm, and zero detectable pathogen load. This water is completely safe for cooling tower makeup, flushing, landscaping, and boiler feedwater pre-treatment.
Q5. What is the expected project execution timeline for an STP or ETP in Silchar?
Pre-engineered modular skids (10 KLD to 100 KLD) are delivered, installed, and commissioned within 3 to 5 weeks. Larger site-erected civil and mechanical plants (200 KLD to 2 MLD) typically require 8 to 12 weeks, depending on civil tank availability and piping layout readiness at your Meherpur Industrial Estate facility.
Q6. Does Trity Environ provide ongoing maintenance and AMC support across Assam?
Yes. We support all installations with dedicated Annual Maintenance Contracts (AMC) and Operations & Maintenance (O&M) programs across Silchar and throughout Assam. Our services encompass periodic water testing, dosing chemical replenishment, preventive pump servicing, membrane chemical washes, and 24/7 technical breakdown support.
CATALOGUE
Related Engineering Products
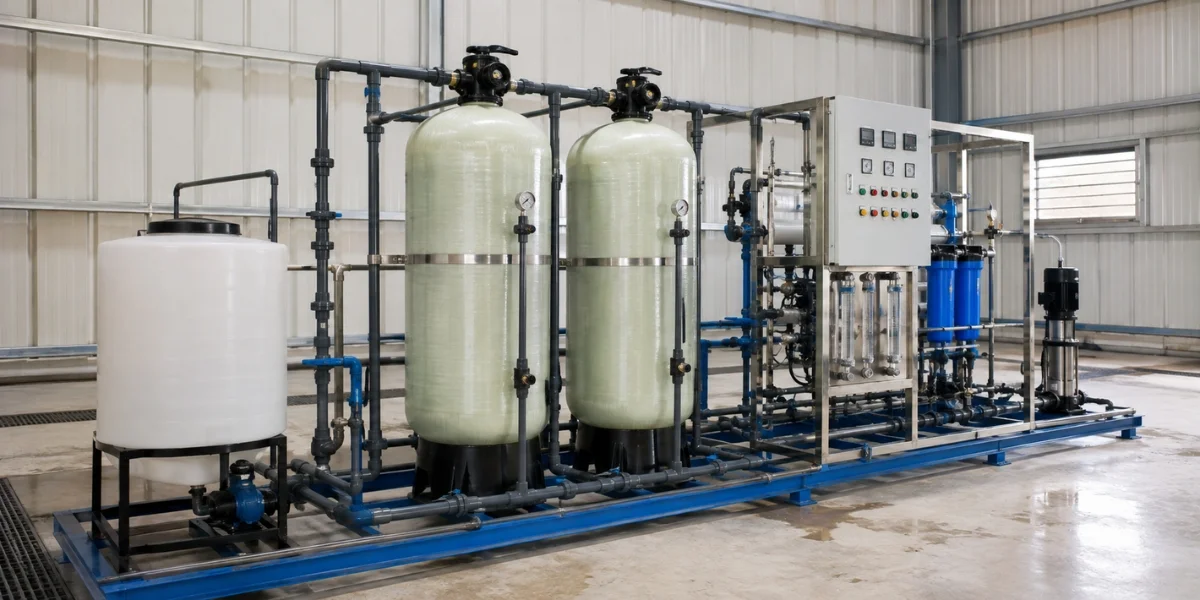
RO & Water Recycling Plant Manufacturer in India
Trity Environ Solutions manufactures RO and water recycling systems for industries and commercial facilities, engineered for reliable purity and reuse.
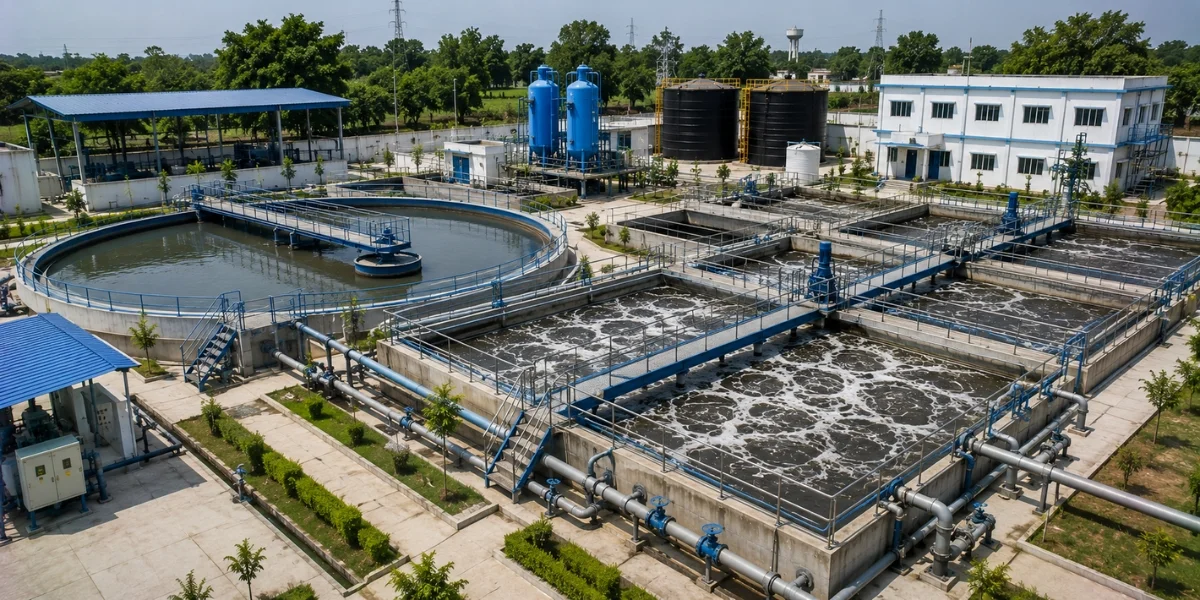
Tertiary Treatment Plant Manufacturer in India
Trity Environ Solutions manufactures tertiary treatment plants that polish treated water beyond secondary treatment, enabling genuine reuse and stricter discharge compliance.
Wastewater Recycling System Manufacturer in India
Trity Environ Solutions manufactures wastewater recycling systems using UF and RO technology, turning treated wastewater into reuse-grade water for cooling, flushing, and gardening.
PAN-INDIA CAPABILITIES
Regional Solutions & State Coverage
TECHNICAL KNOWLEDGE
Related Insights & Engineering Guides
PROVEN EXCELLENCE
Featured Turnkey Installations



Need a Custom Water or Wastewater Treatment Solution?
Our engineering team can help design the right system for your capacity, industry, and compliance requirements.