Step-by-Step Process of a Water Treatment Plant
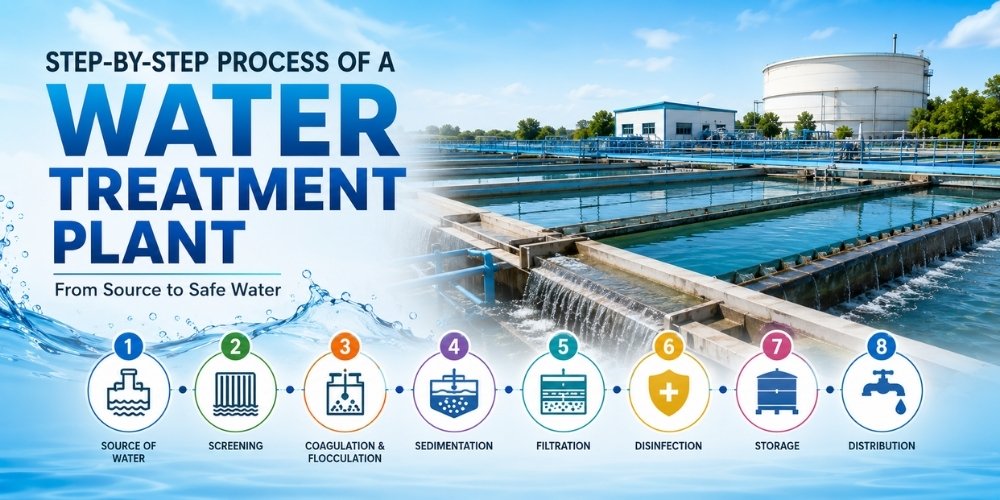
Learn the complete step-by-step process of a water treatment plant, including screening, coagulation, sedimentation, filtration, disinfection, sludge handling, and compliance standards.

 ISO 9001:2015 & QCI Approved
The membrane gets the credit, but it is only one stage of an RO plant. Pretreatment, pumping, chemical dosing and cleaning decide whether that membrane performs for years or fails within months.
In natural osmosis, water moves through a semi-permeable membrane from a weaker solution toward a stronger one. Reverse osmosis flips that direction by applying pressure higher than the solution's osmotic pressure.
The membrane lets water molecules pass and rejects dissolved salts, ions and most larger molecules. Every RO plant therefore produces two streams: permeate, which is the purified water, and reject (also called concentrate), which carries the contaminants left behind.
Everything else in the plant exists to make that single separation reliable. The sections below follow the water through each stage.
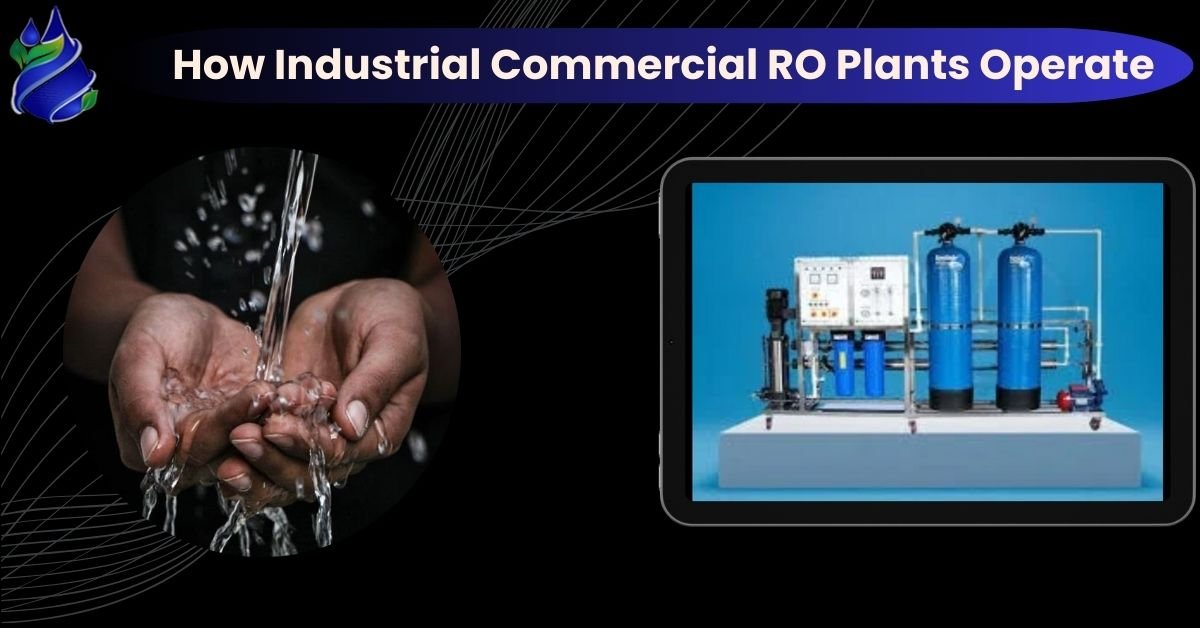
A typical plant follows this path: raw water, pretreatment, 5 micron cartridge filter, antiscalant dosing, high-pressure pump, RO membranes, then permeate and reject.
Raw water is never fed straight to the membrane. Pretreatment is tailored to the feed water, and without it the whole process suffers:
The standard check on pretreatment quality is the Silt Density Index (SDI), which measures how fouling-prone the water is. Membrane makers commonly ask for a low SDI, often below 5, before water reaches the membrane.
Two protective steps sit directly ahead of the pump:
Scale is one of the main reasons membranes lose output, so antiscalant dosing is not an optional extra.
The high-pressure pump supplies the force that overcomes osmotic pressure:
Higher salinity and higher recovery both raise the pressure needed, which is why seawater plants sit at the top of the range.
This is where purification happens:
Recovery is simply permeate flow divided by feed flow. For example, a plant fed at 20 m/hr with 75% recovery produces 15 m/hr of permeate and 5 m/hr of reject.
Permeate usually needs a final adjustment before use:
The process is the same, but the engineering around it changes with scale and duty:
| Aspect | Commercial RO Plant | Industrial RO Plant |
|---|---|---|
| Typical users | Hotels, hospitals, offices, schools | Manufacturing, power, pharma, food and beverage |
| Capacity | Small to mid range | Published industrial specs commonly run from about 10,000 to over 500,000 GPD |
| Construction | Often FRP or stainless steel | Stainless steel, frequently 316L, built for harsh environments |
| Duty cycle | Daily demand with peaks | Continuous 24/7 operation |
| Feed water | Municipal or moderate-TDS borewell | Brackish water up to roughly 15,000 ppm TDS in some designs |
| Control | Basic to PLC | PLC with HMI, often SCADA and remote access |
These figures come from manufacturer-published specifications and are indicative; your own feed water analysis decides the actual design. For specifics, see our pages on the commercial RO plant and industrial RO plant.
The reject stream leaves the membranes still carrying much of the pumping pressure. Energy recovery devices (ERDs) such as pressure exchangers and turbochargers capture it and reuse it:
Our guide on innovations in RO plant technology covers newer membrane and energy-saving developments.
A healthy RO plant is one whose numbers are tracked every day:
Two normalised readings give the earliest warning. A falling normalised permeate flow points to fouling, and a falling normalised salt rejection points to membrane degradation.
When performance drops, clean-in-place (CIP) restores it without dismantling the system:
1. Initial rinse to remove loose dirt
2. Acid cleaning to dissolve scale such as calcium carbonate and calcium sulfate
3. Intermediate rinse to flush and neutralise the acid
4. Alkaline cleaning to remove organic fouling and biofilm
5. Final rinse to clear all cleaning chemicals
6. Disinfection, only when required and compatible with the membrane
The purpose is to restore permeate flow, reduce pressure drop, stabilise salt rejection and extend membrane life.
RO plants serve a wide range of applications, and the design priorities change with each:
Our guide on how reverse osmosis combats water pollution covers the recycling and pollution-control side in more detail.
| Application | Key Stage to Get Right | Why It Matters |
|---|---|---|
| Hotels and hospitals | Pretreatment and remineralisation | Taste, safety and equipment protection |
| Power and boiler feed | Multi-stage RO plus polishing | Boiler scale and corrosion control |
| Food and beverage | Consistent permeate quality | Product consistency |
| Wastewater recycling | Membrane pretreatment, CIP schedule | Fouling control on difficult feed |
Trity Environ Solutions is an experienced industrial RO plant manufacturer and commercial RO plant manufacturer in India, and our engineering team designs the whole train, from pretreatment to post-treatment, around your feed water analysis. As a trusted RO plant manufacturer and supplier, we specify the right combination of multi grade filtration, carbon, softening and ultrafiltration so the membrane is protected from day one. For plants that need ultra-pure output, our demineralized water plant range completes the line.
Every plant is backed by pan-India operation and maintenance support, including scheduled CIP and consumable replacement. We are ISO 9001:2015 certified, QCI approved, and deliver CPCB-compliant engineering nationwide.
Learn the complete step-by-step process of a water treatment plant, including screening, coagulation, sedimentation, filtration, disinfection, sludge handling, and compliance standards.
Protect industrial equipment with advanced water softening. Boost efficiency, cut downtime, and reduce costs with tailored softening solutions.
10 practical, effective ways to reduce water pollution in India, from household habits to industrial treatment and policy-level infrastructure investment.



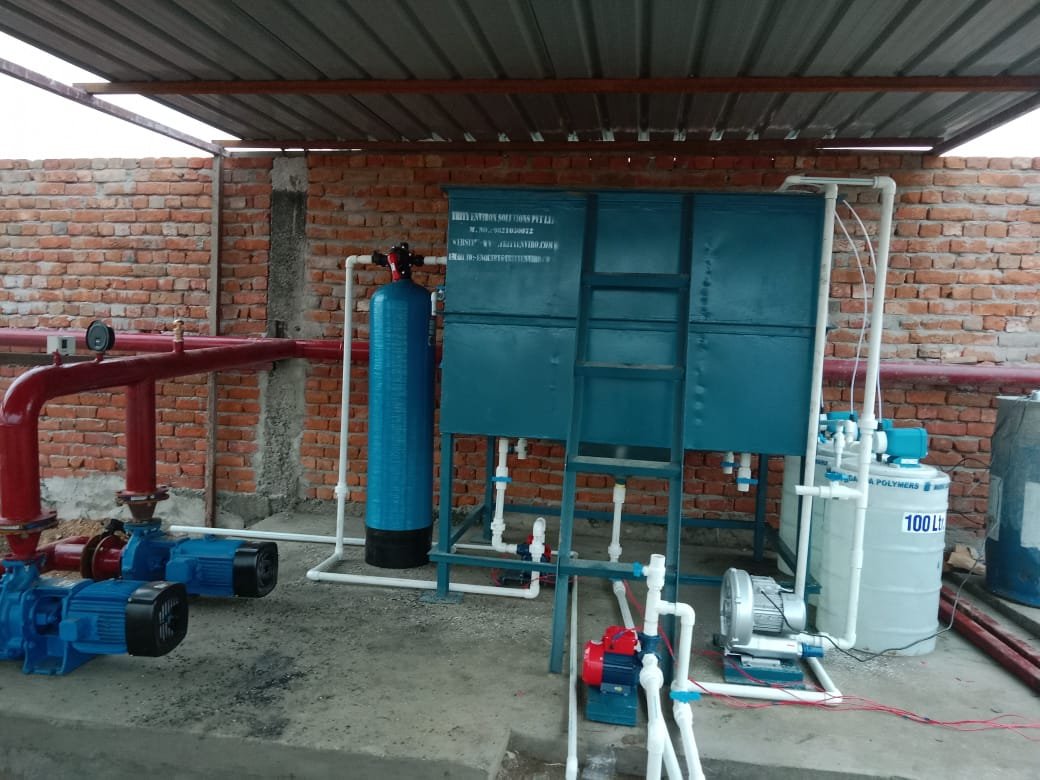
Discuss your requirements with our engineering team and get practical guidance for your project.