Top 3 Commercial RO Plant Manufacturers in Delhi
Looking for a reliable commercial RO plant manufacturer in Delhi? Compare the top 3 companies, their capacity range, services, and how to choose the right one.

 ISO 9001:2015 & QCI Approved
Real innovations reshaping DM water plant technology: electrodeionization, RO-EDI hybrid systems, resin-wafer EDI, and AI-driven optimization. What's changed and why it matters.
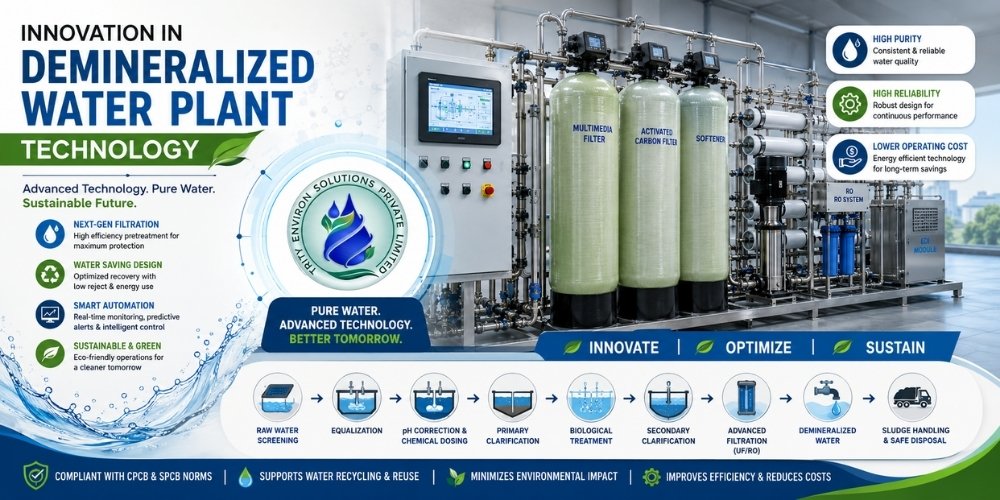
Most articles on demineralized water plant technology describe the same thing: ion exchange resin beds, acid and caustic regeneration, and reverse osmosis membranes. That's accurate, but it's also roughly forty years out of date as a description of where the technology is actually headed. The real shift happening in DM water plant design right now isn't about explaining ion exchange better. It's about reducing or eliminating the chemical regeneration that traditional ion exchange depends on, and the technology driving that shift, electrodeionization, is already standard in semiconductor fabs, power plants, and pharmaceutical facilities worldwide.
A demineralization plant, sometimes called a deionization plant, removes mineral ions, calcium, magnesium, sodium, and other dissolved salts, from water to produce a level of purity ordinary filtration can't achieve. Industries that can't tolerate trace minerals in their process water, semiconductor fabrication, pharmaceutical manufacturing, power generation, and precision electronics among them, depend on this level of purity to protect both product quality and equipment.
Two approaches have historically dominated: ion exchange, where water passes through resin beads that swap mineral ions for hydrogen and hydroxyl ions, and membrane filtration, primarily reverse osmosis, which separates water molecules from dissolved ions using a semipermeable membrane. Both remain in active use today. What's changed is what happens after that first stage, and increasingly, what replaces resin-based ion exchange altogether.
Conventional mixed-bed ion exchange works well, but it carries a genuine operational cost that often gets glossed over in basic explainers. Resin beds saturate with mineral ions over time and need regeneration, typically using concentrated hydrochloric acid and sodium hydroxide at 2 to 8 percent concentration by weight. That means a facility running traditional DM plants has to store, handle, and dispose of hazardous regeneration chemicals continuously, along with managing downtime while regeneration takes place and treating the resulting waste brine before discharge.
For industries where water demand doesn't pause, this creates a real bottleneck. It's also the exact problem the industry's most significant recent innovation was built to solve.
Electrodeionization (EDI) combines ion exchange resins, ion-selective membranes, and an applied DC electric field to remove ionized species from water continuously, without ever stopping for chemical regeneration. Instead of acid and caustic dissolving and flushing out accumulated ions, an electric current drives ions through selective membranes into a separate concentrate stream, while the resin inside the EDI module regenerates itself electrochemically as water flows through.
The practical result is water quality that rivals or exceeds traditional mixed-bed output: conductivity below 0.1 microsiemens, silica below 10 parts per billion, and sodium below 10 parts per billion in well-designed systems. DuPont, one of the technology's major suppliers, positions EDI specifically for semiconductor fabrication and power applications where this level of consistency matters most. Veolia highlights the same core advantage from a different angle: lower operating cost, reduced chemical handling, and a stronger environmental and safety profile compared to chemically regenerated ion exchange.
What makes EDI genuinely different from traditional demineralization:
EDI isn't a replacement for the entire treatment train, though. It works as a polishing stage after reverse osmosis, and it needs stricter feedwater quality than a conventional demineraliser would tolerate. Hardness above roughly 0.5 to 2.0 mg/L as calcium carbonate in the feed can scale the concentrating chambers and cause the system to underperform, which is why proper RO pretreatment ahead of EDI matters more than it would for standalone ion exchange.
The practical innovation most facilities are actually adopting isn't EDI alone, it's RO-EDI hybrid systems that combine reverse osmosis, carbon dioxide degassing membranes, and electrodeionization into a single, factory-tested, skid-mounted unit. Suppliers like Envirogen and WesTech now build these as plug-and-play systems specifically to reduce installation complexity and shorten commissioning timelines.
A typical RO-EDI train works like this: reverse osmosis removes the bulk of dissolved ions and organics first, a CO2 degassing membrane strips dissolved carbon dioxide that would otherwise interfere with EDI performance, and the EDI module handles final polishing to ultrapure standards, all without a single regeneration chemical entering the process. Modern systems pair this with PLC and HMI-based automation and secure, credentialed operator access, which turns what used to require constant manual oversight of resin exhaustion and regeneration cycles into a monitored, largely self-managing process.
Research published in 2025 points to where EDI technology is headed next, and it's a genuinely active area of development rather than a mature, settled technology.
Resin-wafer EDI (RW-EDI) restructures the resin bed into a wafer format that improves modularity and allows more compact, process-intensified system designs, useful for facilities with limited installation space. Membrane-free EDI (MF-EDI) removes one of the more expensive and failure-prone components of conventional EDI, the ion-selective membranes themselves, while aiming to preserve the chemical-free continuous operation that makes EDI valuable in the first place.
Perhaps more significant for day-to-day operation is the integration of AI-driven parameter optimization. Current density, resin bed structure, and flow rate all affect EDI performance, and researchers are now applying machine learning to tune these parameters dynamically rather than relying on fixed setpoints. Early results point toward intelligent systems operating in a genuinely low energy range, roughly 0.1 to 0.3 kilowatt-hours per unit of treated water, alongside advanced electroactive membrane materials that improve ion selectivity and durability.
EDI is also proving useful well beyond standard demineralization. Recent research has demonstrated over 99.8 percent removal efficiency for heavy metals including chromium, nickel, and cadmium, and applications in radioactive wastewater treatment, both signs that the underlying electrochemical approach has real potential outside the semiconductor and power-generation applications it's best known for today.
This isn't a niche upgrade a handful of facilities are experimenting with. According to industry data from SEMI, global semiconductor manufacturing equipment billings reached 135.1 billion dollars in 2025, up 15 percent year on year, with continued fab construction momentum expected through 2027. Ultrapure water is indispensable to chip fabrication, and EDI is already embedded in most high-purity polishing schemes serving this industry. As semiconductor capital investment climbs, so does structural demand for the ultrapure water infrastructure that supports it, which is a meaningful part of why EDI adoption has moved from a specialised option to something closer to a default choice in new high-purity installations.
Pharmaceutical manufacturing, power generation boiler feedwater, and precision electronics assembly are following a similar trajectory, driven by the same underlying logic: chemical-free, continuous, consistently high-purity water production reduces both operational risk and long-term cost compared to managing a chemical regeneration cycle indefinitely.
|
Most articles on demineralized water plant technology describe the same thing: ion exchange resin beds, acid and caustic regeneration, and reverse osmosis membranes. That's accurate, but it's also roughly forty years out of date as a description of where the technology is actually headed. The real shift happening in DM water plant design right now isn't about explaining ion exchange better. It's about reducing or eliminating the chemical regeneration that traditional ion exchange depends on, and the technology driving that shift, electrodeionization, is already standard in semiconductor fabs, power plants, and pharmaceutical facilities worldwide. What a Demineralized Water Plant Actually DoesA demineralization plant, sometimes called a deionization plant, removes mineral ions, calcium, magnesium, sodium, and other dissolved salts, from water to produce a level of purity ordinary filtration can't achieve. Industries that can't tolerate trace minerals in their process water, semiconductor fabrication, pharmaceutical manufacturing, power generation, and precision electronics among them, depend on this level of purity to protect both product quality and equipment. Two approaches have historically dominated: ion exchange, where water passes through resin beads that swap mineral ions for hydrogen and hydroxyl ions, and membrane filtration, primarily reverse osmosis, which separates water molecules from dissolved ions using a semipermeable membrane. Both remain in active use today. What's changed is what happens after that first stage, and increasingly, what replaces resin-based ion exchange altogether. The Real Limitation of Traditional Ion ExchangeConventional mixed-bed ion exchange works well, but it carries a genuine operational cost that often gets glossed over in basic explainers. Resin beds saturate with mineral ions over time and need regeneration, typically using concentrated hydrochloric acid and sodium hydroxide at 2 to 8 percent concentration by weight. That means a facility running traditional DM plants has to store, handle, and dispose of hazardous regeneration chemicals continuously, along with managing downtime while regeneration takes place and treating the resulting waste brine before discharge. For industries where water demand doesn't pause, this creates a real bottleneck. It's also the exact problem the industry's most significant recent innovation was built to solve. Electrodeionization: The Core Innovation Reshaping DM PlantsElectrodeionization (EDI) combines ion exchange resins, ion-selective membranes, and an applied DC electric field to remove ionized species from water continuously, without ever stopping for chemical regeneration. Instead of acid and caustic dissolving and flushing out accumulated ions, an electric current drives ions through selective membranes into a separate concentrate stream, while the resin inside the EDI module regenerates itself electrochemically as water flows through. The practical result is water quality that rivals or exceeds traditional mixed-bed output: conductivity below 0.1 microsiemens, silica below 10 parts per billion, and sodium below 10 parts per billion in well-designed systems. DuPont, one of the technology's major suppliers, positions EDI specifically for semiconductor fabrication and power applications where this level of consistency matters most. Veolia highlights the same core advantage from a different angle: lower operating cost, reduced chemical handling, and a stronger environmental and safety profile compared to chemically regenerated ion exchange. What makes EDI genuinely different from traditional demineralization:
EDI isn't a replacement for the entire treatment train, though. It works as a polishing stage after reverse osmosis, and it needs stricter feedwater quality than a conventional demineraliser would tolerate. Hardness above roughly 0.5 to 2.0 mg/L as calcium carbonate in the feed can scale the concentrating chambers and cause the system to underperform, which is why proper water softening and RO pretreatment ahead of EDI matters more than it would for standalone ion exchange. RO-EDI Hybrid Systems: Two Technologies, One SkidThe practical innovation most facilities are actually adopting isn't EDI alone, it's RO-EDI hybrid systems that combine reverse osmosis, carbon dioxide degassing membranes, and electrodeionization into a single, factory-tested, skid-mounted unit. Suppliers like Envirogen and WesTech now build these as plug-and-play systems specifically to reduce installation complexity and shorten commissioning timelines. A typical RO-EDI train works like this: reverse osmosis removes the bulk of dissolved ions and organics first, a CO2 degassing membrane strips dissolved carbon dioxide that would otherwise interfere with EDI performance, and the EDI module handles final polishing to ultrapure standards, all without a single regeneration chemical entering the process. Modern systems pair this with PLC and HMI-based automation and secure, credentialed operator access, which turns what used to require constant manual oversight of resin exhaustion and regeneration cycles into a monitored, largely self-managing process. What's Coming Next: Beyond Standard EDIResearch published in 2025 points to where EDI technology is headed next, and it's a genuinely active area of development rather than a mature, settled technology. Resin-wafer EDI (RW-EDI) restructures the resin bed into a wafer format that improves modularity and allows more compact, process-intensified system designs, useful for facilities with limited installation space. Membrane-free EDI (MF-EDI) removes one of the more expensive and failure-prone components of conventional EDI, the ion-selective membranes themselves, while aiming to preserve the chemical-free continuous operation that makes EDI valuable in the first place. Perhaps more significant for day-to-day operation is the integration of AI-driven parameter optimization, building on the same advanced sensor technology now reshaping wastewater monitoring more broadly. Current density, resin bed structure, and flow rate all affect EDI performance, and researchers are now applying machine learning to tune these parameters dynamically rather than relying on fixed setpoints. Early results point toward intelligent systems operating in a genuinely low energy range, roughly 0.1 to 0.3 kilowatt-hours per unit of treated water, alongside advanced electroactive membrane materials that improve ion selectivity and durability. EDI is also proving useful well beyond standard demineralization. Recent research has demonstrated over 99.8 percent removal efficiency for heavy metals including chromium, nickel, and cadmium, and applications in radioactive wastewater treatment, both signs that the underlying electrochemical approach has real potential outside the semiconductor and power-generation applications it's best known for today. Why Demand for This Technology Is AcceleratingThis isn't a niche upgrade a handful of facilities are experimenting with. According to industry data from SEMI, global semiconductor manufacturing equipment billings reached 135.1 billion dollars in 2025, up 15 percent year on year, with continued fab construction momentum expected through 2027. Ultrapure water is indispensable to chip fabrication, and EDI is already embedded in most high-purity polishing schemes serving this industry. As semiconductor capital investment climbs, so does structural demand for the ultrapure water infrastructure that supports it, which is a meaningful part of why EDI adoption has moved from a specialised option to something closer to a default choice in new high-purity installations. Pharmaceutical manufacturing, power generation boiler feedwater, and precision electronics assembly are following a similar trajectory, driven by the same underlying logic: chemical-free, continuous, consistently high-purity water production reduces both operational risk and long-term cost compared to managing a chemical regeneration cycle indefinitely. EDI Versus Traditional Ion Exchange: A Practical Comparison
Neither technology has fully replaced the other, and for many facilities, the practical answer isn't choosing one over the other but combining them correctly, RO for bulk removal, EDI for continuous polishing, with traditional mixed-bed ion exchange still relevant as a final safety-net stage in some ultra-critical applications. The Environmental and Cost Case for Chemical-Free DemineralizationBeyond the technical performance numbers, there's a genuinely practical reason EDI adoption keeps accelerating: the total cost and regulatory burden of managing hazardous regeneration chemicals has been rising steadily, and eliminating that burden changes the economics of a DM plant over its operating lifetime, not just its day-to-day running cost. A traditional ion exchange system running continuously generates a steady stream of concentrated acid and caustic regenerant waste that needs neutralisation and, in many jurisdictions, formal disposal documentation before discharge. That's not a one-time capital expense, it's an ongoing operational and compliance cost that scales with production volume. Facilities operating under tightening state pollution control board norms, where regenerant discharge increasingly falls under the same scrutiny as general industrial effluent, are finding that the compliance overhead of chemical regeneration is no longer a minor line item. EDI sidesteps this almost entirely. Without acid and caustic regeneration, there's no regenerant waste stream requiring neutralisation, no chemical storage tanks needing periodic inspection, and no transport and handling risk associated with concentrated hazardous chemicals arriving on-site regularly. For a facility already managing broader compliance obligations, whether that's a pharmaceutical plant under CPCB's Red Category classification or a semiconductor fab with its own strict environmental reporting requirements, removing one entire category of hazardous chemical management from the operation has value that goes beyond the water treatment budget line. The trade-off worth understanding honestly:
None of these are reasons to avoid the technology. They're reasons to plan for it properly rather than assuming a straightforward swap from one demineralization method to another. How to Evaluate Whether Your Facility Is Ready for EDI or RO-EDIA few practical questions help clarify whether upgrading makes sense right now, or whether conventional ion exchange still fits your situation better. What does your current feedwater quality actually look like? If your source water carries high, variable hardness, you'll need to budget for more robust softening and RO pretreatment ahead of any EDI stage, not just the EDI module itself. Skipping this step is the single most common reason EDI installations underperform their rated output. How much does downtime actually cost you? For a facility where a few hours of regeneration downtime barely registers operationally, the continuous-operation advantage of EDI matters less than it does for a semiconductor fab running around the clock, where any interruption to ultrapure water supply can affect an entire production batch. What's your realistic timeline for return on the higher capital investment? Facilities with high water throughput and correspondingly high chemical consumption under a conventional system tend to see the operating cost savings from EDI accumulate faster than lower-throughput operations, where the payback period can stretch out considerably. Do you have, or can you build, the operational expertise EDI needs? This matters more than most vendors emphasise upfront. A well-designed EDI system run by operators unfamiliar with its specific maintenance needs will underperform a properly maintained conventional system, even though EDI's theoretical performance ceiling is higher. For a facility evaluating new demineralization infrastructure, the practical questions have shifted. It's no longer just "how much capacity do I need," but increasingly: how much do you want to reduce chemical handling and hazardous waste management, how important is continuous operation versus tolerating scheduled regeneration downtime, and how tight are your actual purity requirements. A facility running standard industrial rinse water doesn't need EDI-grade output and may be well served by conventional ion exchange at lower capital cost. A semiconductor or pharmaceutical facility, where trace contamination has real consequences, increasingly can't justify not moving toward EDI-based or RO-EDI hybrid systems. Industries Where These Innovations Matter Most
Frequently Asked Questions1. Is electrodeionization actually chemical-free, or does it just use less chemicals than ion exchange?EDI is genuinely chemical-free in operation. Electricity is the only consumable involved in regenerating the resin inside an EDI module, unlike conventional ion exchange, which requires ongoing acid and caustic supply for regeneration. 2. Can EDI replace reverse osmosis entirely?No. EDI is typically used as a polishing stage after reverse osmosis, not as a replacement for it. RO handles the bulk removal of dissolved ions and organics, while EDI brings the water to ultrapure standards that RO alone doesn't achieve. 3. Does EDI work with any feedwater quality?No. EDI systems need stricter feedwater quality than conventional ion exchange demineralizers, particularly around hardness, typically below 0.5 to 2.0 mg/L as calcium carbonate. Proper pretreatment, usually including RO, is necessary to prevent scaling in the EDI module's concentrating chambers. 4. Is EDI more expensive than traditional ion exchange?Upfront capital cost for EDI-based systems is generally higher than conventional ion exchange, but operating costs are typically lower over time due to eliminated chemical purchasing, handling, storage, and hazardous waste disposal. The right choice depends on your facility's purity requirements and operating cost priorities over the system's lifetime. 5. What industries benefit most from switching to EDI or RO-EDI hybrid systems?Semiconductor manufacturing, pharmaceutical production, and power generation see the clearest benefit, given their combination of strict purity requirements and continuous production schedules where regeneration downtime carries a real operational cost. 6. Are resin-wafer EDI and membrane-free EDI available commercially yet?These remain largely research and early-adoption stage technologies as of 2026, showing strong potential in published research for improved modularity and reduced component failure points, but standard EDI and RO-EDI hybrid systems remain the commercially mature choice for most facilities today. Looking to upgrade your facility's water demineralization system, or evaluate whether an EDI or RO-EDI hybrid setup makes sense for your purity requirements? Get in touch or explore our Demineralized Water Plant range. |
||||||||||||||||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
Neither technology has fully replaced the other, and for many facilities, the practical answer isn't choosing one over the other but combining them correctly, RO for bulk removal, EDI for continuous polishing, with traditional mixed-bed ion exchange still relevant as a final safety-net stage in some ultra-critical applications.
Beyond the technical performance numbers, there's a genuinely practical reason EDI adoption keeps accelerating: the total cost and regulatory burden of managing hazardous regeneration chemicals has been rising steadily, and eliminating that burden changes the economics of a DM plant over its operating lifetime, not just its day-to-day running cost.
A traditional ion exchange system running continuously generates a steady stream of concentrated acid and caustic regenerant waste that needs neutralisation and, in many jurisdictions, formal disposal documentation before discharge. That's not a one-time capital expense, it's an ongoing operational and compliance cost that scales with production volume. Facilities operating under tightening state pollution control board norms, where regenerant discharge increasingly falls under the same scrutiny as general industrial effluent, are finding that the compliance overhead of chemical regeneration is no longer a minor line item.
EDI sidesteps this almost entirely. Without acid and caustic regeneration, there's no regenerant waste stream requiring neutralisation, no chemical storage tanks needing periodic inspection, and no transport and handling risk associated with concentrated hazardous chemicals arriving on-site regularly. For a facility already managing broader compliance obligations, whether that's a pharmaceutical plant under CPCB's Red Category classification or a semiconductor fab with its own strict environmental reporting requirements, removing one entire category of hazardous chemical management from the operation has value that goes beyond the water treatment budget line.
The trade-off worth understanding honestly:
None of these are reasons to avoid the technology. They're reasons to plan for it properly rather than assuming a straightforward swap from one demineralization method to another.
A few practical questions help clarify whether upgrading makes sense right now, or whether conventional ion exchange still fits your situation better.
What does your current feedwater quality actually look like? If your source water carries high, variable hardness, you'll need to budget for more robust softening and RO pretreatment ahead of any EDI stage, not just the EDI module itself. Skipping this step is the single most common reason EDI installations underperform their rated output.
How much does downtime actually cost you? For a facility where a few hours of regeneration downtime barely registers operationally, the continuous-operation advantage of EDI matters less than it does for a semiconductor fab running around the clock, where any interruption to ultrapure water supply can affect an entire production batch.
What's your realistic timeline for return on the higher capital investment? Facilities with high water throughput and correspondingly high chemical consumption under a conventional system tend to see the operating cost savings from EDI accumulate faster than lower-throughput operations, where the payback period can stretch out considerably.
Do you have, or can you build, the operational expertise EDI needs? This matters more than most vendors emphasise upfront. A well-designed EDI system run by operators unfamiliar with its specific maintenance needs will underperform a properly maintained conventional system, even though EDI's theoretical performance ceiling is higher.
For a facility evaluating new demineralization infrastructure, the practical questions have shifted. It's no longer just "how much capacity do I need," but increasingly: how much do you want to reduce chemical handling and hazardous waste management, how important is continuous operation versus tolerating scheduled regeneration downtime, and how tight are your actual purity requirements. A facility running standard industrial rinse water doesn't need EDI-grade output and may be well served by conventional ion exchange at lower capital cost. A semiconductor or pharmaceutical facility, where trace contamination has real consequences, increasingly can't justify not moving toward EDI-based or RO-EDI hybrid systems.
EDI is genuinely chemical-free in operation. Electricity is the only consumable involved in regenerating the resin inside an EDI module, unlike conventional ion exchange, which requires ongoing acid and caustic supply for regeneration.
No. EDI is typically used as a polishing stage after reverse osmosis, not as a replacement for it. RO handles the bulk removal of dissolved ions and organics, while EDI brings the water to ultrapure standards that RO alone doesn't achieve.
No. EDI systems need stricter feedwater quality than conventional ion exchange demineralizers, particularly around hardness, typically below 0.5 to 2.0 mg/L as calcium carbonate. Proper pretreatment, usually including RO, is necessary to prevent scaling in the EDI module's concentrating chambers.
Upfront capital cost for EDI-based systems is generally higher than conventional ion exchange, but operating costs are typically lower over time due to eliminated chemical purchasing, handling, storage, and hazardous waste disposal. The right choice depends on your facility's purity requirements and operating cost priorities over the system's lifetime.
Semiconductor manufacturing, pharmaceutical production, and power generation see the clearest benefit, given their combination of strict purity requirements and continuous production schedules where regeneration downtime carries a real operational cost.
These remain largely research and early-adoption stage technologies as of 2026, showing strong potential in published research for improved modularity and reduced component failure points, but standard EDI and RO-EDI hybrid systems remain the commercially mature choice for most facilities today.
Looking to upgrade your facility's water demineralization system, or evaluate whether an EDI or RO-EDI hybrid setup makes sense for your purity requirements? Get in touch or explore our Demineralized Water Plant range.
Looking for a reliable commercial RO plant manufacturer in Delhi? Compare the top 3 companies, their capacity range, services, and how to choose the right one.
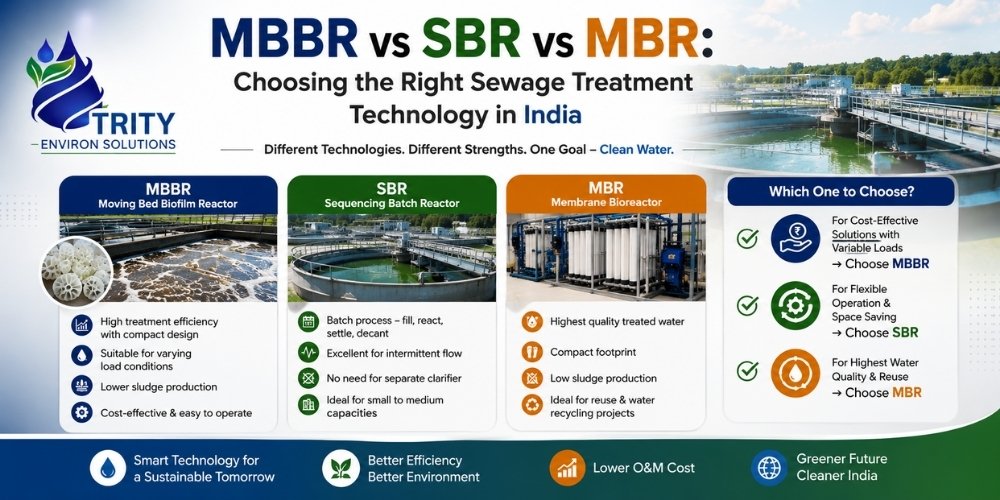
Compare MBBR, SBR, and MBR sewage treatment technologies on footprint, cost, effluent quality, and O&M. Find the right fit for your plant capacity and industry.
Compact STP – Compact Sewage Treatment Plant for efficient wastewater treatment in residential, commercial and industrial applications. Space-saving, cost-effective and easy to install solutions.

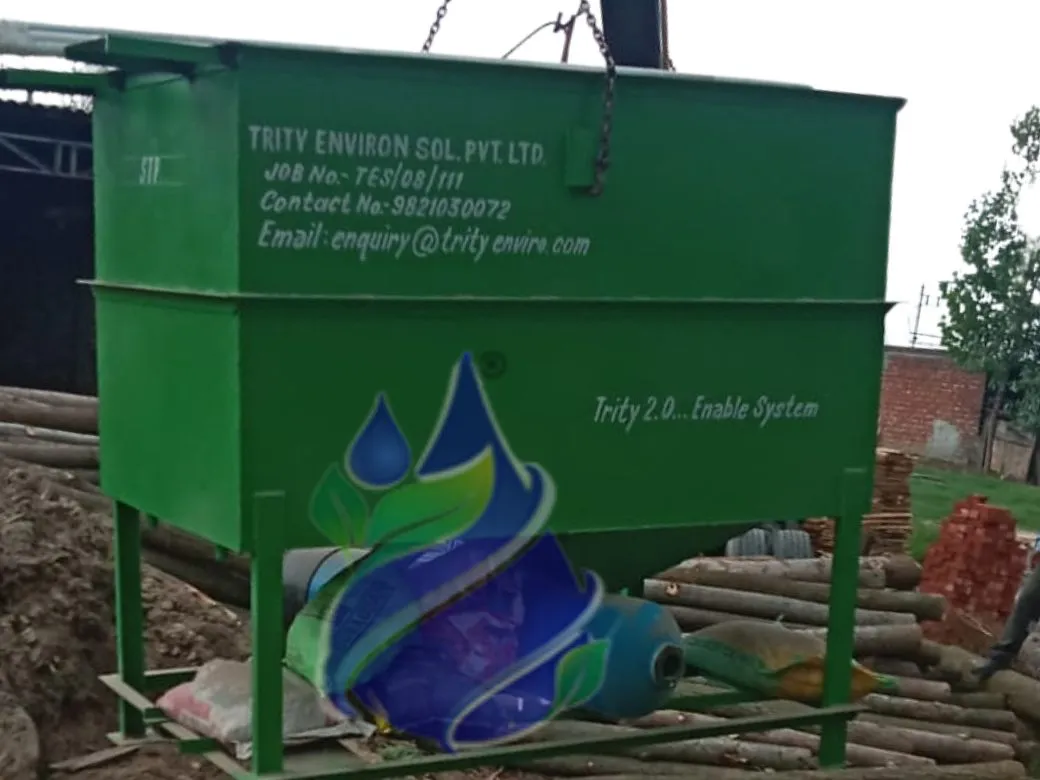
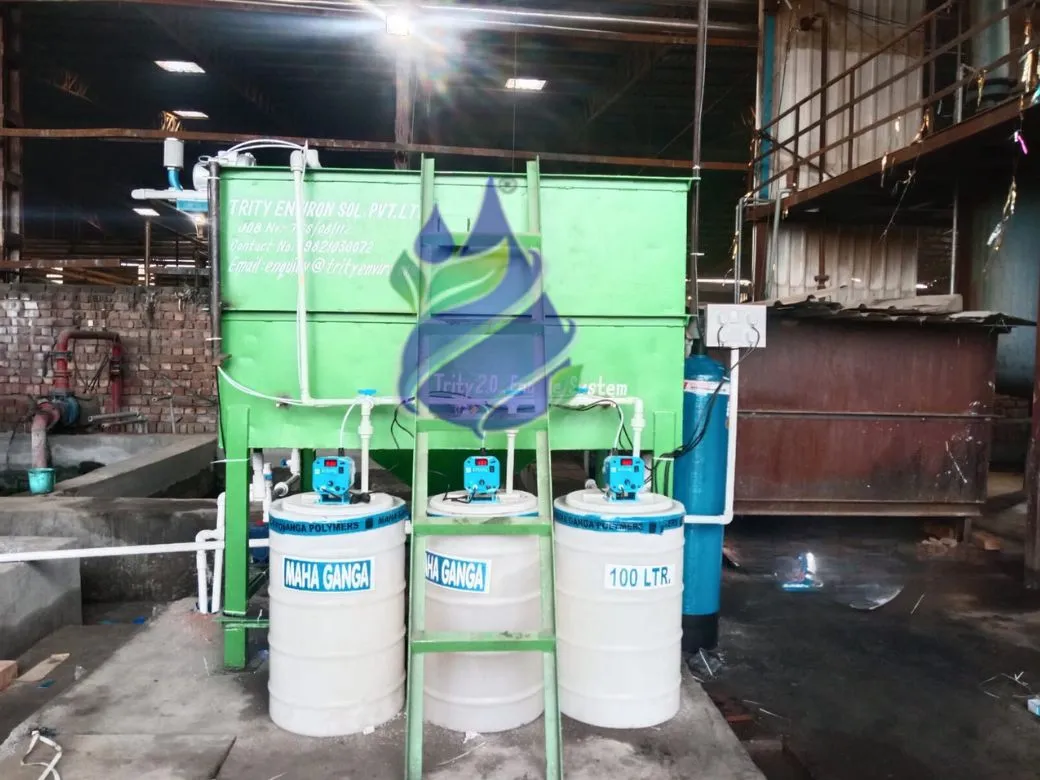


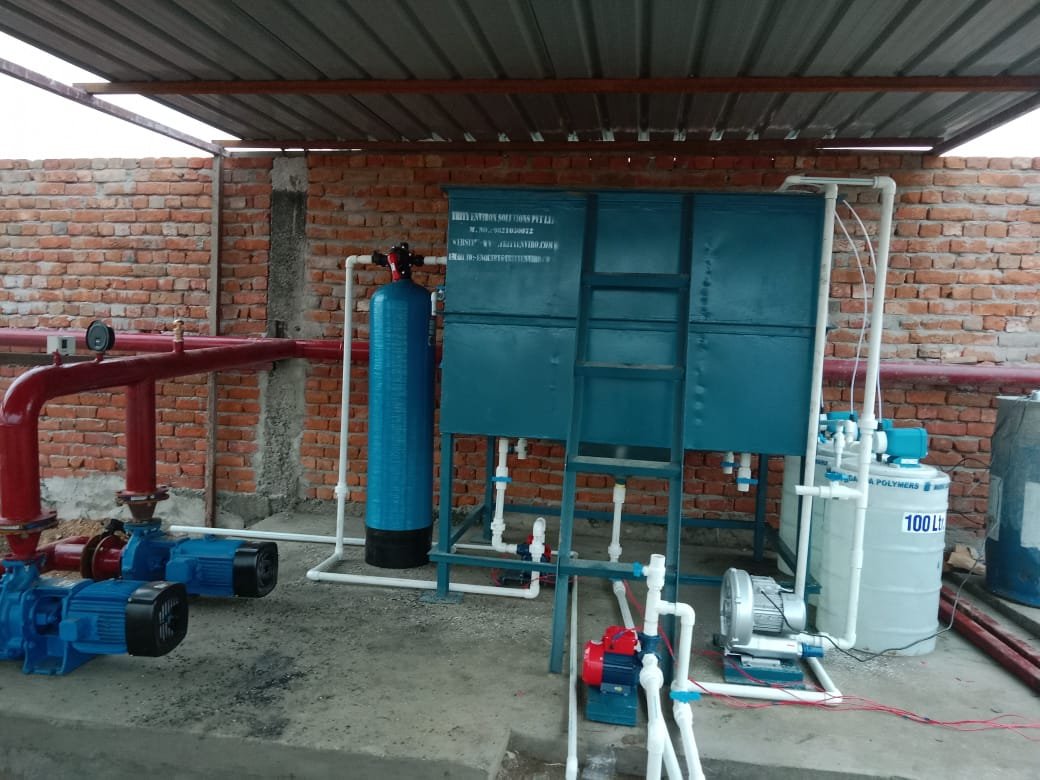
Discuss your requirements with our engineering team and get practical guidance for your project.